If you’ve ever worked as a home appliance stamping parts supplier, you know that even a 1% efficiency gain in your stamping process can translate to thousands of dollars in annual savings, fewer material scraps, and happier customers — all of which make the difference between growing your business and staying competitive. For the last 12 years, I’ve run a small stamping parts plant that makes components for top-tier fridge, washing machine, and oven brands, and optimizing the layout of our stamped parts has been the single most impactful change we’ve made to lower costs and improve quality. Today, I’m pulling back the curtain on the exact, practical steps we use to tweak layouts, cut waste, and keep production running smoothly for home appliance clients. Home Appliance Stamping Parts
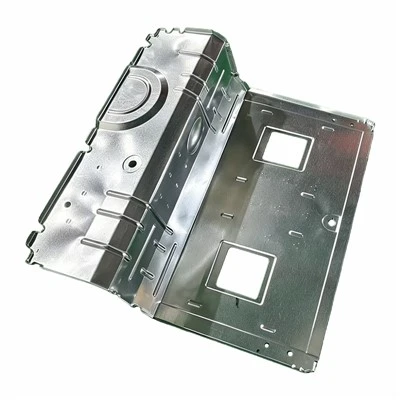
First, let’s get one thing straight: stamping part layout isn’t just rearranging shapes on a sheet of metal. For home appliance stamping parts specifically, every layout choice ties back to customer requirements, material type, and machine constraints. Most of the parts we make are thin-gauge steel or aluminum for appliance door liners, rack supports, control panel brackets, and water dispenser clips. A common mistake new suppliers make is prioritizing maximum parts per sheet over other critical factors, like part durability, tool wear, and the unique quirks of common sheet metals. After all, a layout that packs 12 refrigerator brackets onto a 4×8 steel sheet is useless if 3 of those parts crack during stamping because of poor edge placement.
Start with the Basics: Map Part Requirements Before Touching a Layout
Before we even open our CAD layout software, we spend 24 hours reviewing every detail of the part order with our engineering and quality teams. This step is non-negotiable because home appliance stamping parts have extremely tight tolerances — often ±0.1mm — and surface finish rules that go beyond just fitting on a sheet. For example, a control panel bracket for a wall oven can’t have any sharp burrs on the front side, since it’s visible to the end user. That means when we lay out these parts, we have to account for the stamping direction: the side facing up in the layout will be the finished side, so we arrange parts to avoid burrs on that face, and leave burrs on the underside where they’ll be hidden when the part is assembled.
We also pull the material spec from every order. Most appliance stamping parts use either cold-rolled steel (CRS) for structural components or aluminum alloy 5052 for parts that need to resist rust, like washing machine drain clips. Aluminum has a higher springback rate than steel, meaning it bends back slightly after stamping, so the layout has to account for that. If we lay out two 90-degree bent aluminum clips too close to each other, the springback from adjacent parts will collide and damage edges, leading to 10% higher scrap rates. Last year, we adjusted our layout for a set of dishwasher rack clips by adding a 5mm gap between parts made from 0.8mm aluminum, and scrap from springback dropped from 8% to less than 1%.
Use Nesting Software — But Don’t Let It Replace Your Experience
Nesting software (the tools that arrange parts on a sheet to minimize leftover material, called scrap) is a game-changer, but it’s not a set-it-and-forget-it solution. We use two main tools: SigmaNest for standard structural parts and a custom in-house script for small, high-volume parts like control panel fasteners. The software will typically give you a layout that uses 72-75% of the sheet material for appliance parts, but we almost always tweak that by 2-3% to account for machine limits and part quality.
For example, last quarter we got an order for 50,000 range control panel brackets. SigmaNest’s initial layout packed 11 parts per 4×8 sheet, with a material yield of 74.2%. But when we tested a sample run, the software’s layout put the brackets too close to the edge of the sheet, where the stamping die’s pilot holes (used to align the sheet) couldn’t hold the metal securely, leading to 2mm of misalignment on 3% of parts. We manually shifted the layout inward by 10mm, which brought the part count down to 10 per sheet, but increased yield to 75.8% — that’s a net gain, not a loss, because fewer misaligned parts meant we didn’t waste extra sheets re-stamping bad units. The software didn’t catch that edge alignment issue, but our team’s knowledge of stamping press capabilities did.
Another trick we use with nesting software: for large parts like fridge door inner liners, we leave a small gap around each part to make it easier to remove the stamped part from the die. Large liners have complex, curved edges, and if they’re too tight to adjacent parts, the stripping process (pushing the part out of the die) can bend or scratch the liner’s smooth inner surface, which would make it unfit for use. For liners, we adjust the layout to give a 8mm gap between parts, even if the software could fit an extra liner per sheet. The few extra sheets we use are offset by zero scrap from damaged liners.
Design Layouts to Reduce Tool Wear and Downtime
Home appliance stamping production runs are usually high-volume, often 10,000+ parts per order, so anything that slows down the press or wears out tools adds up. Layout choices directly impact tool life, and we learned this the hard way a few years ago. We were stamping a line of water dispenser brackets, and our tooling was wearing out 20% faster than the industry average — the cost of new die sets was cutting into our profit margin.
After inspecting the die and the layout, we noticed a pattern: all the bracket parts were arranged so their bent legs were facing the same direction. When the die stamped 10,000 parts in a row, the die’s bend punch was rubbing against the same small area of the sheet every time, causing uneven wear. We flipped half the parts in each layout so their bent legs alternated direction, which spread the load across the entire punch face. Tool life increased by 35%, and we cut die replacement costs by $12,000 that year.
Another layout tweak for tool wear: avoid placing sharp corners of adjacent parts directly across from each other in the die. When the press stamps, the sharp corner of one part creates a tiny amount of extra pressure on the die’s corresponding point, leading to micro-cracks that grow over time. For our oven control brackets, which have small, 1mm radius corners, we adjust the layout to offset each part’s corners by at least 15mm from the corner of any adjacent part, which reduces die stress and extends die life.
Account for Material Gauge and Grain Direction
Material grain direction is a detail that many new stamping suppliers overlook, but it’s critical for appliance parts, especially ones that need to bend without cracking. Most steel and aluminum sheets are rolled in one direction, so they have a grain that runs along the length of the sheet. If you stamp a part so its bend line is perpendicular to the grain, it’s far more likely to crack than if the bend line is parallel.
For example, our washing machine drum mounting brackets require a 180-degree bend to fit around the drum. When we first started stamping these, we arranged the brackets with their bend lines perpendicular to the sheet’s grain, and 5% of the brackets cracked during bending. We adjusted the layout to rotate each bracket 90 degrees so the bend line ran parallel to the grain, and cracking dropped to less than 0.5%. The software doesn’t always flag grain direction issues automatically, so our team always adds a grain direction layer to our CAD files before nesting, and we cross-check every layout against that layer.
Material gauge also plays a role in layout. Thin-gauge parts (under 0.5mm) like control panel clips can be arranged more tightly, with smaller gaps between parts, because they’re less likely to deform during stamping. Thicker parts (over 2mm) like structural brackets for fridge doors need larger gaps, because thicker metal requires more force to stamp, and there’s more chance of adjacent parts colliding during the process. Last year, we switched from 1mm to 1.5mm steel for a line of dishwasher frame brackets, and we had to increase the layout gap from 6mm to 10mm — even though that reduced parts per sheet by one, the scrap rate from deformed thick metal dropped by 40%.
Post-Layout Testing: Never Skip the Sample Run
No matter how good your CAD layout looks, you have to run a small sample of parts to check for issues. For every new layout we create, we stamp a trial run of 50 parts, then inspect them for burrs, cracks, misalignment, and dimensional accuracy. We also test the parts for fit with the customer’s product — even if the layout is perfect, a part that doesn’t fit a fridge door slot is useless.
Last month, we got an order for custom microwave door latches. Our initial layout looked great on paper, with 15 parts per sheet and 76% yield. But during the sample run, we noticed that the latch’s spring tab was bending 0.5mm more than it was supposed to. The software had accounted for material springback, but only for flat parts, not the small, thin spring tab. We adjusted the layout by moving each latch 2mm away from the edge of the sheet, which gave the die more room to form the tab without pulling extra material, and the tab’s bending depth was perfect. That sample run saved us from stamping 50,000 defective parts, which would have cost us over $8,000 in rework and penalties.
Final Tip for Layout Optimization: Iterate With Your Customers
At the end of the day, we optimize layouts to meet our customers’ needs, not just our own. Most appliance brands have specific requirements for scrap levels, lead times, and part dimensions, so we work with their engineering teams to tweak layouts when needed. For example, a few months ago, a major fridge brand asked us to adjust the layout of their door liner parts to use 100% recycled aluminum for sustainability goals. Our initial layout used virgin aluminum, but we worked with their team to adjust the part’s edge shape slightly, which allowed us to use recycled aluminum without increasing scrap rates. The new layout not only met their sustainability requirements but also gave them a 5% lower part cost, which led to a two-year contract renewal.
If you’re a home appliance manufacturer looking to cut costs, reduce scrap, and improve the quality of your stamping parts, getting the layout right is one of the fastest ways to do it. We’ve spent years refining these steps, and they’ve helped us grow our business by 30% over the last three years, while keeping our defect rate below 0.8% — which is well below the industry average of 2.5%.
Single Stage Dies & Gang Dies If you need help optimizing your home appliance stamping parts layout, or if you’re looking for a reliable supplier that understands the unique requirements of appliance stamping, feel free to reach out to our team to discuss your project. We’re always happy to walk through our process, test a sample layout, and find solutions that work for your production needs.
References
- Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems (7th ed.). Wiley.
- Kalpakjian, S., & Schmid, S. R. (2019). Manufacturing Processes for Engineering Materials (7th ed.). Pearson.
- Society of Manufacturing Engineers. (2021). Stamping and Forming Processes for Automotive and Appliance Components. SME Press.
- Tavares, P. M., et al. (2018). "Optimization of Nesting Layouts for Stamping Processes with Material and Tool Constraints." Journal of Manufacturing Systems, vol. 47, pp. 192-201.
- Home Appliance Manufacturers Association. (2022). Quality Standards for Stamped Metal Components in Major Appliances. HAMA Technical Bulletin No. 12.
Dongguan Changdong Tool & Die Co., Ltd.
With abundant experience, we are one of the most reliable home appliance stamping parts manufacturers and suppliers in China. Please feel free to buy advanced home appliance stamping parts made in China here from our factory. Good service and quality products are available.
Address: No. 56-B, Fumin South Road, Dalang Town, Dongguan City, Guangdong Province, China
E-mail: sales@stamping-die.com
WebSite: https://www.metalstampingdie.com/
